Confirm the instrument-truck supply boundary
Define the selected tools, line and deployment method, depth and load basis, acquisition channels and required output records for the actual well program. The proposed truck configuration should identify its carrier, installed deployment equipment, operator workspace and power arrangement. Ask the supplier to list supported interfaces and limitations instead of assuming universal instrument compatibility from the product name.
External wellhead and pressure-control equipment require their own competent selection and acceptance. Surface separators, flow meters and effluent handling are separate package responsibilities unless explicitly included in the accepted offer. Any required data connection to those systems needs an identified interface and verification plan. Retain that boundary with the purchase, factory evidence and site handover records.
Evaluate engineering evidence before marketing claims
A capable test well truck manufacturer should turn your duty data into calculations, drawings, component selections and a clear list of assumptions. Ask the bidder to explain how the proposed package performs mobile instrument deployment, depth measurement and data acquisition for an accepted well-survey program and how it is derated for the destination climate. Generic brochures are useful for orientation, but they are not a substitute for a project-specific technical proposal.
Review experience with comparable applications rather than counting unrelated installations. Useful references state the process duty, operating environment, delivery scope and year. Protect confidential end-user information, but request enough evidence to establish that the supplier understands the equipment and its interfaces.
Factory and quality-system checks
Design control
Check calculations, drawings, revisions and approval responsibilities.
Material traceability
Verify certificates, heat numbers and records for pressure-retaining or critical parts.
Assembly inspection
Use inspection checkpoints for alignment, cleanliness, torque and piping quality.
Functional testing
Agree no-load, load-simulation, alarm, shutdown and leak tests.
For the major assemblies—line-handling and winch arrangement, depth measurement and instrument interfaces, installed power and control arrangement, surface data-acquisition and operator workspace—ask who manufactures each item, who owns the technical selection and how warranty support is coordinated. The integrator must remain accountable for the performance of the complete package.
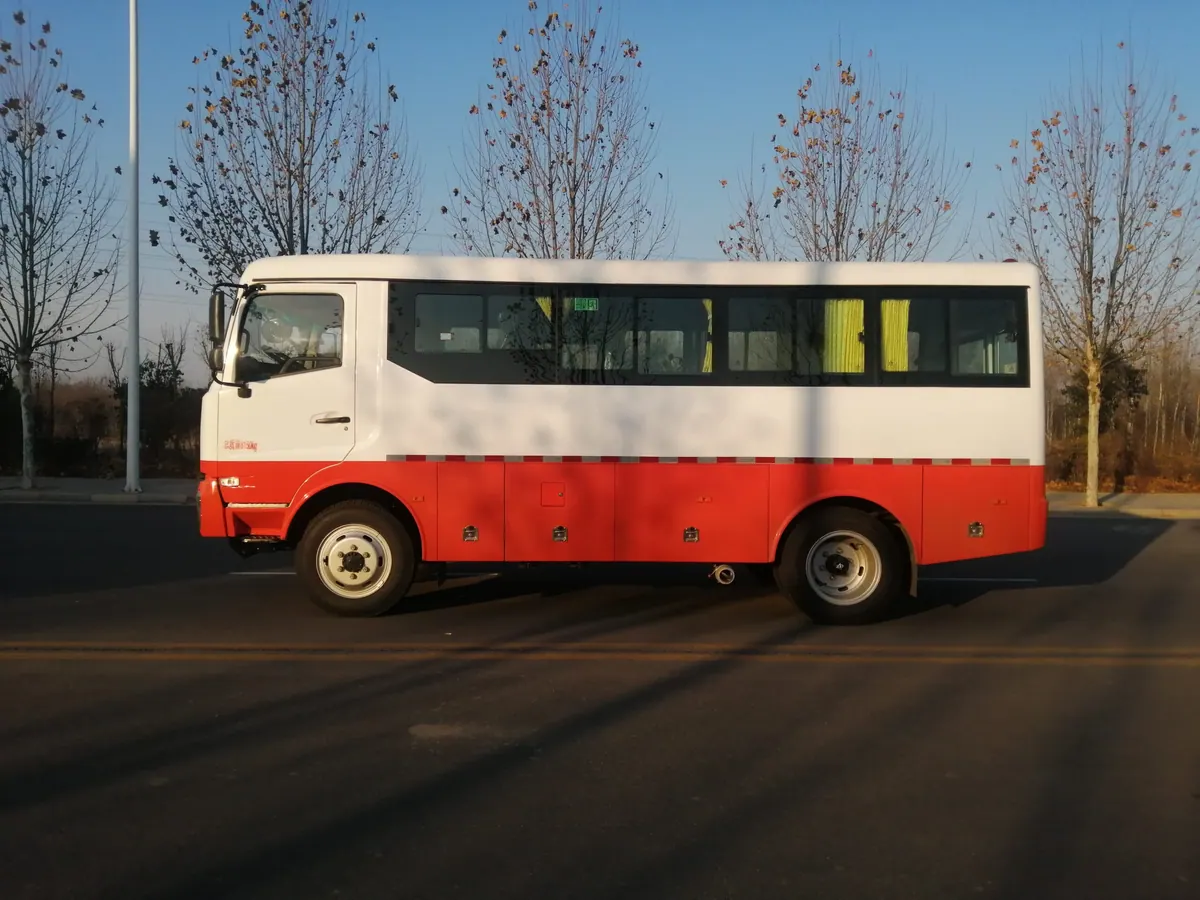
Define the factory acceptance test in the purchase order
| FAT stage | Minimum coverage | Buyer action |
|---|---|---|
| Document review | Approved drawings, data sheets, certificates and software list | Before physical test |
| Mechanical inspection | Dimensions, access, guards, labels, piping and workmanship | Record punch items |
| Functional test | Start, stop, controls, alarms, interlocks and emergency shutdown | Witness critical sequences |
| Performance evidence | Pressure, flow, temperature, power or separation duty as applicable | State test method and tolerance |
If full-load testing is impractical at the factory, agree an alternative: component test certificates, calibrated simulation, partial-load testing and a site performance test. Acceptance criteria must be measurable, not phrases such as “runs normally.”
Documentation and support that reduce startup risk
- General arrangement, foundation and connection drawings
- Process, electrical, hydraulic and pneumatic schematics
- Operation, maintenance and troubleshooting manuals
- Parts list with manufacturer and model references
- Inspection records, calibration certificates and test reports
- Remote support, training, commissioning and warranty process
A reliable manufacturer discusses exclusions and unknowns early. Use a technical bid evaluation table to score compliance, deviations, evidence and lifecycle support before commercial negotiation.
Test Well Truck project-specific engineering focus
A robust procurement package distinguishes mandatory performance from preferred features and future expansion allowances. A supplier review should ask for selection evidence for the line-handling and winch arrangement and depth measurement and instrument interfaces, manufacturing and inspection records for the installed power and control arrangement, and a functional test that proves the surface data-acquisition and operator workspace. The proposal should state how selected tools and line requirements and accepted depth and load conditions were converted into component ratings.
Use the four intended duties as separate review cases: instrument surveys for exploration wells, selected production measurement programs, post-treatment instrument surveys and repeated well-survey campaigns. For each case, record the starting condition, target output, operating duration, expected variation and shutdown condition. This exposes whether a shared configuration is genuinely suitable or whether a different control range, material, auxiliary system or connection set is needed.
line-handling and winch arrangement with depth measurement and instrument interfaces
Review their operating envelopes together. Capacity on one side is not useful if the connected subsystem cannot supply, transmit or control the same duty.
installed power and control arrangement with surface data-acquisition and operator workspace
Define monitoring, protection, calibration and maintenance access as part of the package acceptance criteria rather than optional details.
The RFQ should therefore carry a project data sheet, interface drawing and deviation schedule. That combination gives the manufacturer enough information to explain the design and gives the buyer a consistent basis for technical evaluation, factory testing and later commissioning.
For broader industry context, consult OSHA oil and gas extraction safety guidance. Project requirements and applicable codes must still be confirmed for the destination country and end user.
Frequently asked questions
What should a qualified test well truck manufacturer provide?
Expect project calculations, drawings, component data, a deviation list, quality records, an agreed factory test and complete operation and maintenance documents.
Is a factory acceptance test necessary?
Yes. The FAT verifies workmanship, controls, alarms and agreed performance evidence before shipping, when corrections are easier and less expensive.